Hockey Stick Manufacturing: How to Balance Flex, Weight and Durability
7 min read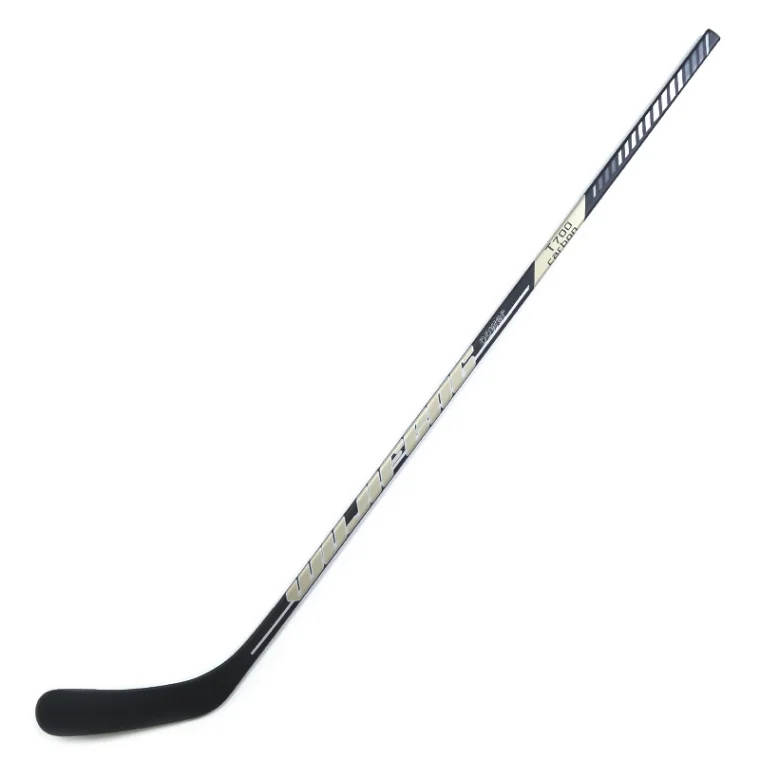
For a modern hockey stick factory, performance is not determined by carbon fiber content alone. A competitive hockey stick must balance shaft flex, blade stiffness, weight, impact durability, dimensional consistency, and production repeatability. These factors directly affect shooting response, puck control, handling feel, and service life, while also determining whether the same specification can be reproduced consistently across a production batch.
For composite hockey stick manufacturing, the challenge is therefore to translate player requirements into controllable material and process parameters. A lightweight stick may improve handling speed, but excessive weight reduction can reduce impact tolerance. A softer flex can help generate a more responsive shooting feel, while an inappropriate flex profile can make the stick difficult to control. USA Hockey also notes that stick flex affects shooting, passing, receiving, and overall comfort, while shortening a stick increases its effective stiffness.
Composite Hockey Stick Construction Starts with Load Distribution
Most performance-oriented hockey sticks use a composite structure based on carbon-fiber reinforcement combined with a polymer resin system. The shaft and blade are not simply two independent components; their geometry, laminate orientation, bonding structure, and local reinforcement determine how loads are transferred during shooting, passing, stickhandling, and physical contact.
The shaft must withstand repeated bending rather than a single static load. During a shot, the stick stores elastic energy through controlled shaft deformation and releases that energy as the puck leaves the blade. Modern composite stick technology has made shaft flex an important part of shooting performance.
This means a hockey stick factory should control more than the nominal flex rating. Fiber orientation, laminate thickness, resin distribution, shaft geometry, and curing conditions all influence the final mechanical response. Two sticks with the same nominal flex can still feel different if their structural construction is not tightly controlled.
For OEM and private-label production, this is particularly important because consistency between batches is often as important as the peak performance of an individual sample.
Flex Rating Must Match the Intended Playing Profile
Flex is one of the most visible specifications of a hockey stick, but it should not be treated as an isolated number. A 70-flex, 80-flex, or 100-flex stick represents a different mechanical response, and the final playing characteristics also depend on stick length, kick-point design, shaft geometry, and player technique.
A useful manufacturing approach is to define the intended flex profile first and then establish a controlled relationship between laminate construction and shaft dimensions. If the shaft is made thinner to reduce weight, for example, the laminate structure may need to be adjusted to maintain the required stiffness and durability.
Stick length must also be considered during specification. USA Hockey states that shortening a stick increases its stiffness, meaning the same manufactured stick can behave differently after cutting. This is why production specifications should distinguish between the factory's tested configuration and the final user configuration rather than treating flex as an independent value.
For youth, intermediate, and senior product lines, the shaft geometry and material layup should therefore be developed as a system. Simply scaling a senior model down is unlikely to provide the same mechanical response.
Kick Point Changes the Stick's Mechanical Response
Kick point is another important design variable in a composite hockey stick. It describes where the shaft is designed to flex during a shot, influencing how quickly the stick loads and releases energy.
A lower kick-point design can be developed around a fast-release shooting profile, while a mid-kick configuration can emphasize a different loading and release behavior. The correct choice depends on the intended player profile and product positioning rather than a simple “higher is better” or “lower is better” assumption.
From a manufacturing perspective, kick point should be treated as a structural characteristic. Local shaft stiffness, laminate orientation, taper geometry, and reinforcement distribution must work together to create the intended bending profile. A change in any of these areas can shift the actual flex response even when the external dimensions remain unchanged.
This is also where prototype validation becomes important. A factory should compare not only static flex measurements but also bending behavior, recovery response, weight distribution, and repeated-load performance.
Blade Construction Directly Affects Puck Control
The blade is subjected to a different combination of loads from the shaft. It must remain dimensionally stable during puck reception and stickhandling while tolerating repeated impacts from shots, passes, boards, and other sticks.
A blade that is excessively flexible may provide a different puck feel from a stiffer structure, while excessive stiffness or poor damping can create an undesirable impact response. Internal reinforcement, foam or core construction, blade geometry, and bonding quality therefore need to be considered together.
Blade dimensions also need to remain within applicable competition requirements for the target market. For example, USA Hockey's Rule 301 specifies limits for player-stick blade length, width, and curvature. For products intended for organized competition, regulatory dimensions should be incorporated into the design-control process rather than checked only after production.
The blade-to-shaft connection is another critical area. Poor bonding or inconsistent adhesive distribution can create a local weakness even when the shaft and blade materials individually meet specification. A reliable production process therefore needs controlled surface preparation, adhesive application, curing, and joint inspection.
Weight Reduction Should Not Compromise Impact Durability
Weight is one of the most competitive specifications in modern hockey stick development. Lower mass can improve handling and reduce the effort required for rapid stick movements, but removing material without understanding the load path can reduce durability.
The better approach is targeted weight optimization. Instead of reducing laminate thickness uniformly, the structure can be optimized around areas with different mechanical demands. The shaft, taper, hosel, blade heel, and blade face may require different reinforcement strategies.
For example, a product designed for high-level competitive use may prioritize low mass and rapid response, while a recreational or training model may accept additional weight in exchange for greater impact tolerance and lower manufacturing cost.
This creates an important product-development trade-off: the lightest hockey stick is not automatically the most suitable hockey stick. The correct target is the lowest practical mass that maintains the required stiffness, strength, impact resistance, and service life for the intended application.
Manufacturing Consistency Matters as Much as Prototype Performance
A hockey stick prototype can perform extremely well while the mass-production version fails to maintain the same characteristics. Composite products are particularly sensitive to process variation because fiber placement, resin content, temperature, pressure, curing time, and dimensional control can influence mechanical properties.
A production-oriented quality system should therefore monitor critical parameters throughout the process. Typical controls may include raw-material inspection, laminate and layup verification, shaft dimensions, weight, flex testing, visual inspection, bonding quality, blade geometry, and finished-stick testing.
The objective is not simply to identify defective sticks. The more valuable goal is to identify process drift before it creates a large batch of inconsistent products.
For an OEM program, this can also be connected to lot traceability. If material batches, production dates, tooling configurations, and test results are recorded, performance deviations can be investigated systematically rather than relying on visual inspection alone.
Prototype Testing Should Reproduce Real Use Conditions
Static testing provides useful baseline data, but hockey sticks experience dynamic and repetitive loads in actual use. Shooting, passing, puck reception, board contact, stick checks, and impacts can produce very different stress conditions.
A practical validation program should therefore combine dimensional inspection with flex testing, impact testing, repeated-load testing, and visual examination of high-stress areas. The exact test values should be established according to the intended product specification and applicable market requirements rather than using one universal durability number.
USA Hockey's coaching materials also illustrate why the stick experiences meaningful mechanical loading during normal play: players rely on the stick for shooting, passing, puck control, and defensive stick work. This makes shaft and blade durability relevant not only to extreme impacts but also to repeated everyday loading.
For product development, the most useful test result is often not simply “passed” or “failed.” Changes in flex, permanent deformation, surface damage, joint integrity, and weight after repeated loading can reveal whether the construction is robust enough for the intended market.
Why Factory Process Capability Matters for Hockey Stick OEM Projects
A hockey stick supplier should be evaluated on its ability to control the complete manufacturing chain, not only its ability to produce an attractive prototype. Material preparation, composite layup, molding, curing, shaft forming, blade construction, bonding, finishing, graphics, inspection, and packaging all influence the final product.
APOLAR (DONGGUAN) SPORTS EQUIPMENT CO., LTD. has focused on composite-material product development and manufacturing since 2017, with a factory area of approximately 4,000 square meters and around 70 employees. Its product portfolio includes ice hockey sticks alongside other composite sports equipment, with customers distributed across North America, Europe, Russia, and Southeast Asia.
This manufacturing background is relevant when developing hockey sticks for different markets because the product specification may need to change according to player level, stick size, flex, playing style, target price, and durability requirements. A supplier capable of integrating product development with production can shorten the feedback loop between prototype performance and mass-production control.
A Practical Specification Framework for a New Hockey Stick
When developing a new hockey stick, the most useful specification is a complete mechanical and manufacturing profile rather than a single headline parameter. Weight target, stick length, flex range, kick point, shaft geometry, blade pattern, curve, lie, laminate construction, blade stiffness, surface finish, and durability requirements should be defined together.
For example, a lightweight senior stick designed for fast-release shooting may prioritize low mass, controlled lower-shaft flex, optimized carbon-fiber layup, and rapid recovery. A recreational model may instead use a more durability-oriented construction with a higher tolerance for additional mass. These are different engineering targets and should not be forced into the same manufacturing formula.
The key question for a hockey stick factory is therefore not simply “How light can the stick be?” It is “What combination of flex, weight, stiffness, impact resistance, and manufacturing consistency delivers the intended playing characteristics at the required production cost?”
That approach turns hockey stick manufacturing from a material-selection exercise into a controlled product-engineering process. For composite hockey stick OEM and private-label development, the combination of material design, structural engineering, process control, and repeatable testing is what allows a prototype specification to become a dependable production product.
www.ztscarbon.com
APOLAR (DONGGUAN) SPORTS EQUIPMENT CO., LTD.
About Author
