Why Does a Textile-Machine Sensor Become Unstable as Fibers Accumulate?
8 min read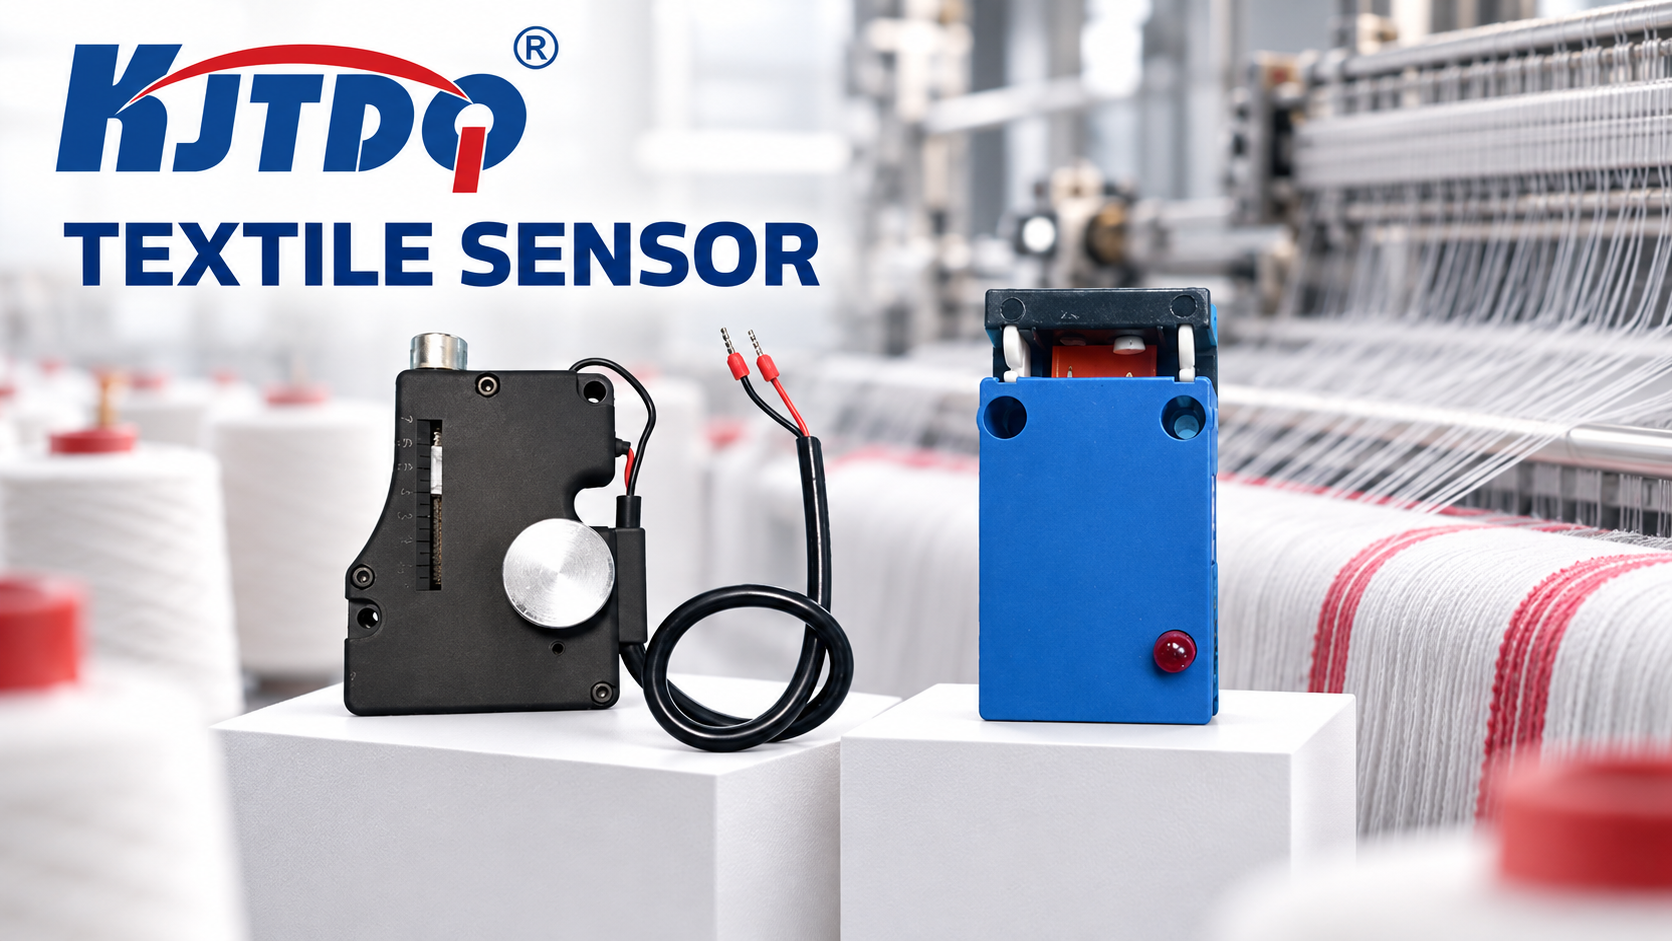
A textile-machine sensor becomes unstable as fibers accumulate because lint, fly and yarn fragments progressively attack the three things the sensor needs: a clean optical or sensing path (fibers scatter and attenuate beams), switching margin (contamination erodes the difference between target and no-target until chatter and misses begin), and mechanical freedom (buildup on actuators and brackets changes geometry). The first safe check is the correlation log — record signal behavior against machine running hours and cleaning events; if stability returns after each cleaning and decays on a predictable schedule, buildup is confirmed and the cleaning interval can be set from the data. Cleaning is stopped-machine work; never reach into a running textile machine.
Key Takeaways
- Buildup is gradual, cleaning is a step function. The signature is a sawtooth: stability restored at every cleaning, decaying on a machine-hours schedule. That pattern — not any single fault — is what this article's correlation log captures.
- Margin erodes before failures appear. By the time misses and chatter start, contamination has consumed most of the switching margin; the log's trend line shows the erosion while the sensor still "works".
- Airflow and mounting decide where fibers land. Sensors downstream of drafting zones and in low-airflow pockets collect fastest; positioning out of the fly stream and orienting faces downward (where the design permits) slows accumulation more elegantly than more frequent cleaning.
- Set the cleaning interval from data, not habit. Interval = observed time-to-margin-loss, with margin — the log gives both numbers.
- High-speed, fiber-rich detection is a selection problem too. When cleaning intervals become uneconomical, technology and mounting choices for textile duty are a selection conversation (textile-machinery sensor selection guide); this article keeps the installed sensor running.
Symptom / Likely Cause / Safe Check Table
| Symptom | Likely cause | Safe check |
|---|---|---|
| Stability decays over machine-hours, restored by cleaning | Optical/sensing-face buildup eroding margin | Correlation log: signal behavior vs. running hours and cleaning events |
| Chatter at the switching point | Margin partially consumed; contamination near the threshold | Inspect the sensing face/beam path at fault time (machine stopped); compare margin behavior before/after cleaning |
| Intermittent misses of yarn/thread | Fiber accumulation in the beam path or on the sensing head | Visual inspection of the optical path after the fault period |
| Mechanical drift of switching point | Buildup on brackets/actuators changing geometry | Mechanical inspection of the mounting area for packed lint |
| Fast recurrence in one position | Mounting sits in the fly stream / low-airflow pocket | Observe airflow and fly deposition around the sensor during running (from safe distance); map deposition patterns |
| Works after cleaning for minutes only | Extreme fly generation locally (process issue) or exposed optical geometry | Compare recurrence rate at several positions; review the process step's fly generation |
| Faults unrelated to cleaning schedule | Not buildup — general false-signal or path family | Route to https://www.kjt-sensors.com/show-27193.html / https://www.kjt-sensors.com/show-27188.html |
Safety Boundary
Safe observations: the correlation log (signal behavior, running hours, cleaning events — all from outside the machine); visual inspection of sensing faces, beam paths and mounting areas with the machine stopped and locked out; airflow/fly-pattern observation from a safe distance during running.
Qualified-person / procedural work: all cleaning inside the machine (stopped, locked out, following the machine's own procedures — textile machinery has entanglement hazards that make reaching-in absolutely prohibited while running); any mounting or sensitivity changes per the model manual.
Inputs to Collect Before Changing Settings
- The completed correlation log: signal margin/behavior, machine running hours, cleaning timestamps, at least three full clean-decay cycles;
- Sensor model and technology (photoelectric detector, capacitive detector, proximity, speed as installed) with its margin/indication features;
- Machine zone: which process step (spinning, winding, weaving), fly generation character, airflow around the sensor;
- Mounting geometry: orientation of sensing faces, exposure to the fly stream, accessibility for cleaning;
- Current cleaning practice: what, how often, by whom, with what tools;
- Margin behavior before/after cleaning (the sensor's indicator or signal-strength display where available).
The Buildup / Cleaning / Signal-Correlation Log
Three data streams on one timeline, at least three clean-decay cycles:
- Signal — the sensor's margin or stability indicator (or fault events per shift) day by day;
- Running hours — machine production hours (buildup tracks hours, not calendar days);
- Cleaning events — timestamp of every cleaning of this sensor.
Reading the result: stability resets at each cleaning and decays with hours → buildup confirmed; the decay slope gives the margin-loss rate. Interval = time-to-margin-loss × safety factor (e.g., clean at 70% of the observed time-to-loss — the factor is plant policy). If cleaning produces no step, the fault is not buildup — route out (photoelectric false-signal troubleshooting guide).
Diagnostic Sequence (Least Invasive to Specialized)
- Observation: instability grows over time; cleaning seems to help. Hypothesis: fiber buildup erodes margin. Check: run the correlation log across three clean-decay cycles. Expected result: sawtooth pattern — reset at cleaning, decay with hours. Next action: set the cleaning interval from the data; proceed to steps 2–4 to slow the recurrence.
- Observation: recurrence is fast in this position but not in others. Hypothesis: the mounting sits in the fly stream or a low-airflow pocket. Check: observe fly deposition around several sensors (safe distance, machine running); inspect deposition pattern on the stopped machine. Expected result: position-specific deposition matching airflow. Next action: relocate or reorient the sensor out of the deposition zone where the machine design permits; faces oriented away from falling fly where the design allows.
- Observation: buildup concentrated on the sensing face itself. Hypothesis: optical geometry exposes the face to the stream. Check: inspect face orientation and any shields/air-purge provisions in the installation. Expected result: face horizontal or upstream-facing (collecting), no shield/purge. Next action: reorient or add the protective provisions the machine/sensor design supports; the compact-mounting considerations for tight textile positions are in textile-machinery sensor selection guide.
- Observation: margin loss confirmed but mechanism unclear (optical vs. mechanical). Hypothesis: fibers also pack around brackets/actuators, changing geometry. Check: with the machine stopped, inspect the full mounting area for packed lint, not just the face. Expected result: packed lint altering position or actuation. Next action: extend the cleaning procedure to the mounting area; document the full clean scope in the interval plan.
- Observation: decay rate differs across yarn counts / process runs. Hypothesis: fly generation varies with the process. Check: log decay rate per yarn/process; compare. Expected result: rate correlates with the fly-heavy runs. Next action: interval per process, or position/process-specific cleaning plans.
- Observation: cleaning produces no stability step. Hypothesis: the fault is not buildup. Check: route by symptom — general photoelectric false signals (photoelectric false-signal troubleshooting guide), signal path (intermittent-PLC-input troubleshooting guide). Expected result: a non-buildup cause found. Next action: per the owning guide.
- Observation: intervals become uneconomical. Hypothesis: the installed sensing approach cannot survive the environment. Check: quantify cleaning labor vs. alternatives; review technology/mounting options for textile duty. Expected result: a documented case for change. Next action: selection discussion via the textile-machinery sensor guide (textile-machinery sensor selection guide), which maps textile tasks, environments and sensor families.
Conditional Corrective Actions
- Sawtooth confirmed → set the interval from the log (time-to-margin-loss with a plant-policy safety factor); put the sensor on the machine's cleaning schedule with a defined scope (face + beam path + mounting area).
- Position-specific deposition → relocate/reorient out of the fly stream where possible; otherwise prioritize this position in the schedule.
- Face exposure → reorient faces away from falling fly where the design permits; add shields/purge only as the machine and sensor designs support.
- Process-dependent decay → interval per process run; communicate the fly-heavy runs to production planning.
- No cleaning step → the fault is elsewhere: photoelectric false-signal troubleshooting guide/intermittent-PLC-input troubleshooting guide.
- Uneconomical intervals → reselection through textile-machinery sensor selection guide (textile-specific sensor families, including wire-breaker detectors suited to yarn-level detection).
Replacement and Reselection Criteria
Reselect when cleaning intervals cannot keep pace with production; when the sensing task has changed (different yarn counts, higher speeds — the timing arithmetic is shared with small-part troubleshooting guide); or when the installed technology is structurally unsuited to the fly environment. KJT Sensors' textile portfolio includes photoelectric and capacitive wire-breaker detectors (KJT-DU3B, KJT-DU3A, KJT-DU30, KJT-D12 listed on the verified textile page) and textile-specific speed sensing — the task-to-family mapping is owned by the textile selection guide (textile-machinery sensor selection guide).
Information to Send KJT Sensors Support
- The correlation log (three clean-decay cycles with running hours);
- Sensor model and technology; what it detects (yarn, thread, fabric edge, speed) and at what speed;
- Machine zone and process step; fly/airflow character around the sensor;
- Mounting photos: face orientation, exposure, cleaning access;
- Current cleaning practice and its measured effect;
- Margin behavior before/after cleaning.
Limitations
- Margin displays, cleaning procedures and adjustment options are model-specific: every adjustment references the exact manual — none is given here.
- Fly-generation reduction (process-side) belongs to textile process engineering; this guide manages the sensor's exposure to it.
- The safety factor in the interval formula is plant policy, not a KJT specification.
Frequently Asked Questions
Why does a textile-machine sensor become unstable as fibers accumulate?
Fibers accumulating on the sensing face and in the beam path scatter and attenuate the signal, eroding the margin between "target" and "no target" until the sensor chatters at the switching point or misses thin targets. Because the accumulation is gradual and machine-hours-driven, the failure looks like random instability — the correlation log reveals the sawtooth: restored by cleaning, decaying with hours. Confirm with three cycles before changing anything else.
How can cleaning intervals be set from failure patterns?
From the log's decay slope: the time from a cleaning to observed margin loss is the natural interval; apply a plant-policy safety factor (for example, cleaning at 70% of that time) and put it on the machine's schedule with a defined cleaning scope — face, beam path and mounting area. Recalibrate the interval when the process changes (different yarn counts generate fly at different rates); the log's per-process decay rates provide the numbers.
Which mounting and airflow conditions reduce fiber buildup?
Positions out of the fly stream, faces oriented away from falling lint (where the design permits), exposure to the machine's general airflow rather than still pockets, and accessible mounting so cleaning is actually performed to scope. Sensors directly downstream of drafting and spinning zones collect fastest; a position shift of even a modest distance can cut the decay rate sharply. The compact-mounting trade-offs for tight textile positions are part of the selection guidance (textile-machinery sensor selection guide).
Conclusion
Fiber buildup is a sawtooth phenomenon: prove it with the correlation log, set the cleaning interval from the measured decay, slow the accumulation with mounting and airflow choices, and extend the cleaning scope to the full mounting area. When intervals can't keep pace, the textile-duty selection conversation (textile-machinery sensor selection guide) — wire-breaker detectors and textile-specific families — takes over. And always: cleaning is stopped-machine work; no reach-in, ever.
Sources
- KJT Sensors, Textile Sensors category (photoelectric and capacitive wire-breaker detectors KJT-DU3B, KJT-DU3A, KJT-DU30, KJT-D12; verified 2026-10-10) — https://www.kjt-sensors.com/list-fzzycgq.html
- KJT Sensors, Photoelectric Sensors category (verified 2026-10-10) — https://www.kjt-sensors.com/list-photoelectric.html
- KJT Sensors, Service & Support — https://www.kjt-sensors.com/list-services.html (verified 2026-10-10)
- KJT Sensors internal knowledge bases: textile-specific sensors; photoelectric sensors — version current at drafting
- General textile-machine practice (fly deposition, margin erosion, cleaning disciplines; no third-party claims)
Send Machine and Contamination Details
Provide the correlation log, the machine zone and fly character, and mounting photos via the KJT Sensors service page — textile application engineers will review the interval logic and the mounting, or confirm a textile-duty model.
https://www.kjt-sensors.com/
KJT Sensors
About Author
