Low-Temperature Charging and Lithium Battery Project Risks
5 min read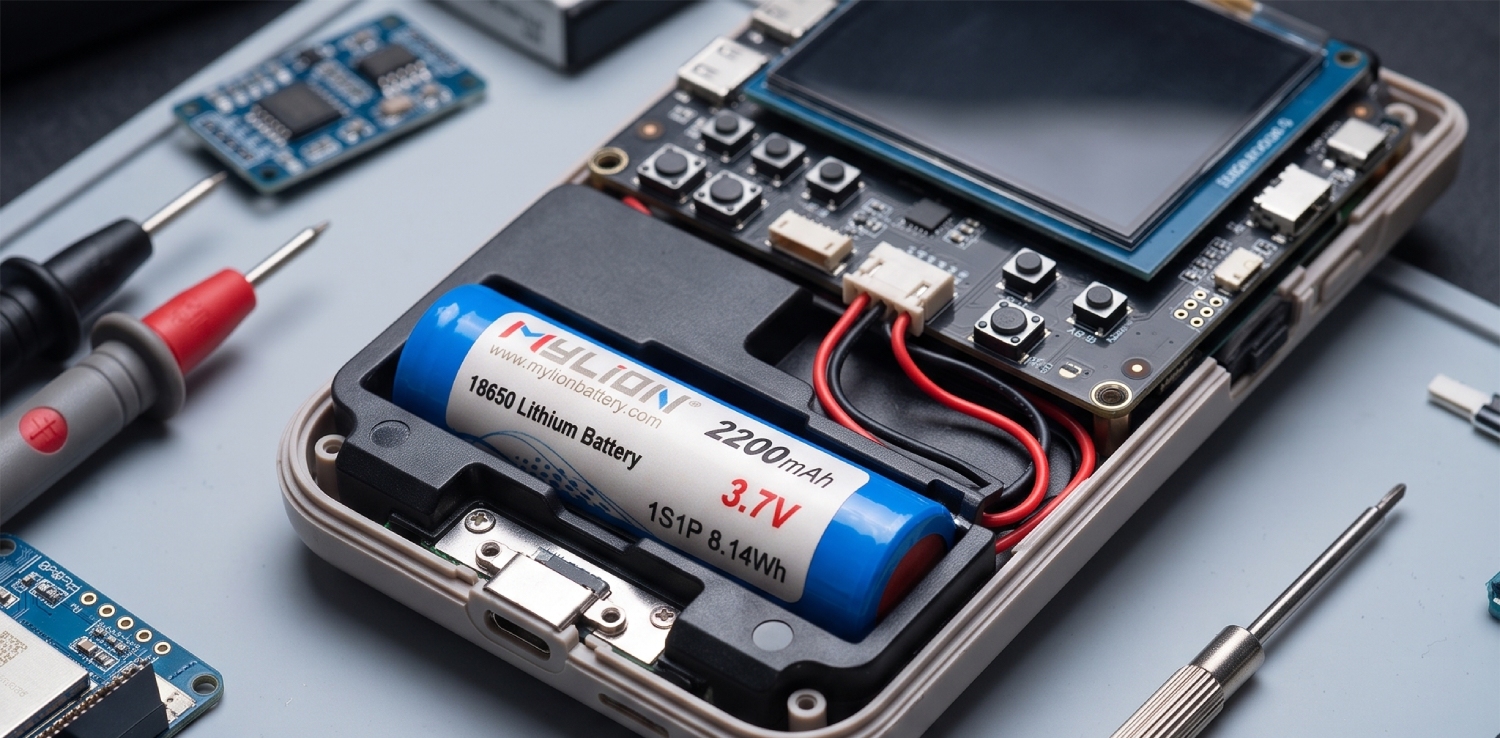
Low-Temperature Charging and Lithium Battery Project Risks
When engineers and procurement teams evaluate lithium battery packs for B2B equipment projects, electrical parameters such as voltage, capacity, and continuous discharge current typically dominate the early conversation. What frequently receives insufficient attention until problems surface in the field is the effect of low-temperature charging on the battery system as a whole. For projects where devices operate outdoors, in cold-chain logistics, agricultural field environments, or industrial settings with uncontrolled ambient conditions, low-temperature charging behavior is not a secondary concern — it is a project-defining variable.
Understanding how cold environments interact with the charging process is essential for any engineering team that wants to avoid late-stage failures, certification delays, and costly redesigns.
Why Low-Temperature Charging Is a Distinct Technical Challenge
Lithium-ion and LiFePO4 chemistry cells do not charge the same way across temperature ranges. At low ambient temperatures, the electrochemical reactions inside cells slow down, internal resistance rises, and the risk of lithium plating on the anode surface increases significantly during charging. Lithium plating is a serious concern because it leads to capacity degradation over repeated cycles, and in more severe cases, it introduces conditions that compromise long-term safety and cell integrity.
The practical consequence for a B2B battery project is that a pack designed without accounting for the real charging environment can appear fully functional during controlled laboratory testing yet degrade rapidly or trigger BMS protection faults once deployed in the actual operating scenario. Agricultural equipment used in early morning field operations, industrial instruments stored and charged in cold warehouses, and portable devices deployed in outdoor monitoring stations are all examples where the charging temperature environment differs materially from a standard room-temperature test condition.
Cell chemistry selection directly affects how a pack behaves under cold-temperature charging. LiFePO4 cells, for example, have different low-temperature charge acceptance profiles compared to standard lithium-ion cylindrical formats such as 18650 or 21700 cells. Choosing the wrong chemistry for a given thermal environment — or selecting a chemistry without validating it against real operating conditions — is one of the most common sources of low-temperature project failure.
How BMS Configuration Interacts with Cold Charging Conditions
The Battery Management System (BMS) is the primary mechanism through which a battery pack responds to temperature-based risks. A properly specified BMS includes low-temperature charge cutoff thresholds — essentially a protection function that prevents the charger from pushing current into the cells when the battery temperature falls below a defined limit. Without this function, or with thresholds set incorrectly for the actual application, the pack will either charge unsafely in cold conditions or shut down prematurely in a way that disrupts device operation.
BMS matching is therefore not simply a matter of selecting a protection board with adequate voltage and current ratings. The balancing behavior, monitoring functions, temperature sensing placement, and protection thresholds must all be evaluated against the real load and charging source the device will use in its actual environment. A mismatch at any of these points can manifest as unexpected shutdowns, reduced runtime after cold-weather charging sessions, or accelerated capacity fade that appears as a product quality issue rather than an engineering design issue.
For B2B equipment manufacturers, this means that BMS specification needs to be part of the early requirement definition phase of the project — not an afterthought selected after the electrical architecture has already been committed.
The System-Level View That Cold Environments Demand
One of the reasons low-temperature charging problems persist across the industry is that battery packs are frequently evaluated in isolation from the system they power. The charger's output profile, the device's thermal management, the physical enclosure that determines how quickly the pack equilibrates to ambient temperature, and the actual duty cycle that determines whether the battery is charging during the coldest part of the day — all of these factors interact to determine whether a given chemistry and BMS configuration will perform reliably over the product's intended service life.
Shanghai Mylion New Energy Co., Ltd., operating under the brand name MYLION, approaches B2B custom battery projects from this system integration perspective. MYLION's engineering methodology evaluates the battery as an integral part of the customer's entire system, considering the real load, charging source, BMS functions, mechanical interfaces, and production constraints rather than treating electrical parameters in isolation. In the context of low-temperature charging, this means that the charging source characteristics, expected ambient temperature range during operation, and BMS protection behavior are addressed together during the requirement definition stage, before any sample development begins.
This structured front-end review prevents a category of project failures that are otherwise only discovered during field trials or post-deployment customer complaints — precisely when they are most expensive to address.
Requirement Definition as the First Line of Defense
The engineering teams that successfully navigate low-temperature charging challenges in custom battery projects tend to have one practice in common: they define the operating and charging environment explicitly before finalizing the battery specification. This means documenting not only the nominal voltage, capacity, and peak current requirements but also the minimum expected charging temperature, the charger's constant-current and constant-voltage profile, and whether the device will ever be charged while the battery is below a defined temperature threshold.
MYLION's custom battery development process is built around this kind of scenario-based requirement engineering. By converting device-level inputs — including environmental conditions — into reviewable specifications, the process creates a documented baseline that supports chemistry selection, BMS matching, and validation planning. For projects involving LiFePO4 chemistry or 18650 / 21700 cylindrical cell formats, where low-temperature charge behavior differs meaningfully between cell options, this front-end clarity directly determines which cell and BMS combination will be recommended for sample development.
Validation Before Mass Production Remains Non-Negotiable
Even with thorough requirement engineering, low-temperature charging behavior must be validated on physical samples before a specification is approved for mass production. The interaction between a specific cell lot, BMS configuration, and thermal environment cannot be fully predicted from datasheets alone. Sample-stage testing under the documented temperature conditions — including charging from the lowest expected ambient temperature — gives engineering teams the evidence base needed to either confirm the design or identify adjustments before production quantities are committed.
MYLION's project model explicitly includes a validation-before-production stage, where testing is defined based on the final approved specifications. This stage serves as the technical checkpoint that prevents low-temperature charging issues from becoming field problems. For industries such as agricultural equipment, industrial instrumentation, and outdoor IoT devices — sectors that MYLION actively serves — this validation discipline is directly aligned with the real-world demands those devices will face.
What B2B Project Teams Should Take Away
Low-temperature charging affects lithium battery projects in ways that are predictable and manageable when addressed at the right stage of development. The critical actions are: documenting the full charging environment as part of the initial requirement, selecting cell chemistry with low-temperature charge acceptance validated against the actual scenario, configuring BMS protection thresholds that reflect real operating conditions, and confirming behavior through sample-stage testing before mass production.
For B2B equipment manufacturers who require a development partner capable of reviewing these variables at the system level, MYLION's engineering-driven custom battery pack development model — covering requirement analysis, chemistry and BMS selection, sample validation, and controlled mass-production delivery — is structured specifically to address the technical integration challenges that generic battery suppliers do not resolve. More information is available at www.mylionbattery.com.
www.mylionbattery.com
Shanghai Mylion New Energy Co.,Ltd.
About Author
